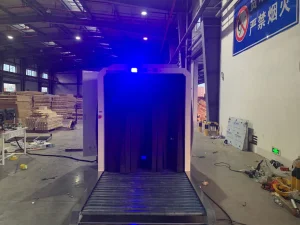
Hangzhou Maith Conveyor Co., Ltd. is a professional manufacturer specializing in warehouse conveyor systems, smart logistics automation equipment, and advanced material handling solutions for global distribution, manufacturing, and e-commerce industries. Established in 2013 and headquartered in Hangzhou, China, the company integrates research and development, system design, precision manufacturing, installation services, and international OEM/ODM support into a complete industrial automation ecosystem.
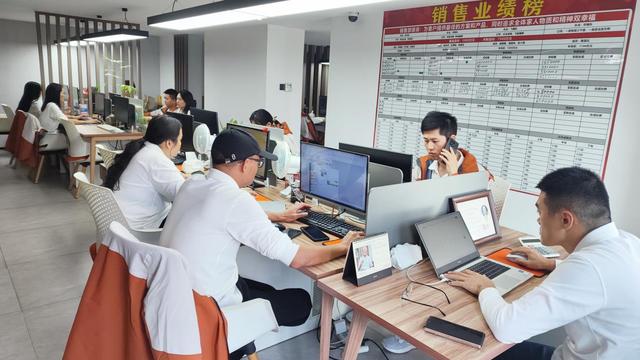
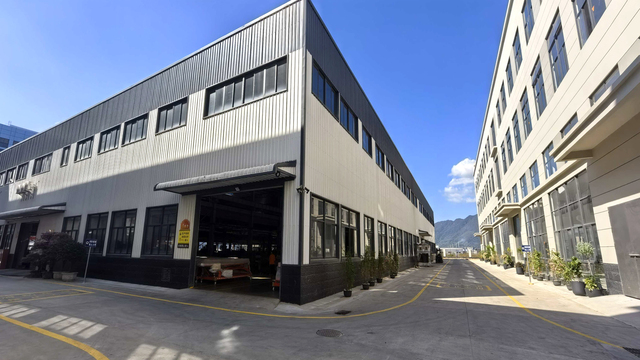
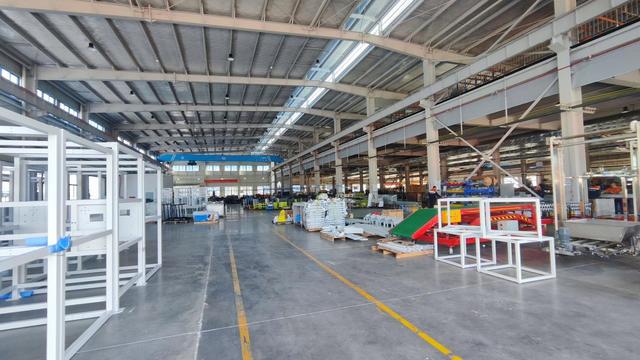
The company operates a modern production base covering approximately 30,000 square meters with more than 360 employees, including mechanical engineers, automation specialists, and software control experts. Equipped with advanced fabrication workshops, automated assembly lines, and rigorous quality inspection systems, Maith Conveyor ensures high performance, stability, and durability across all conveyor solutions. Annual production capacity exceeds 6,500 complete conveyor systems, serving clients in warehousing, logistics centers, airports, retail distribution hubs, manufacturing plants, and fulfillment operations worldwide.
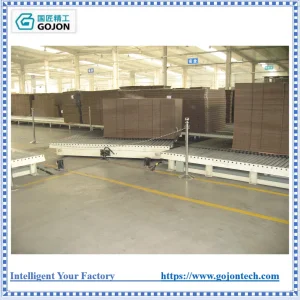
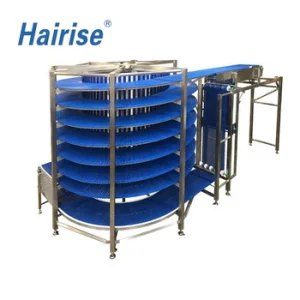
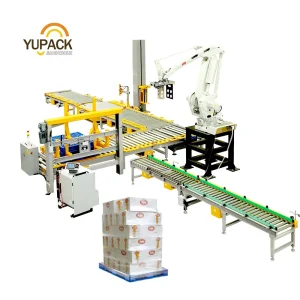
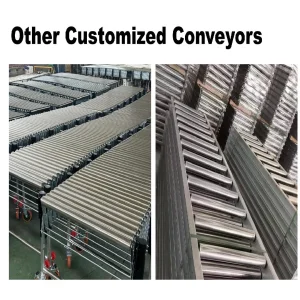
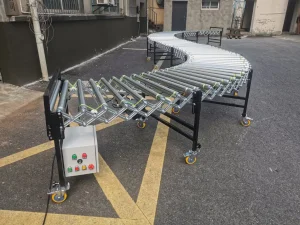
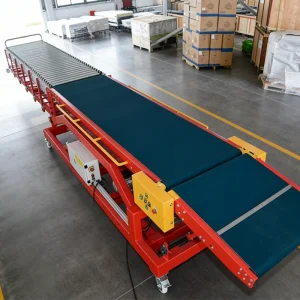
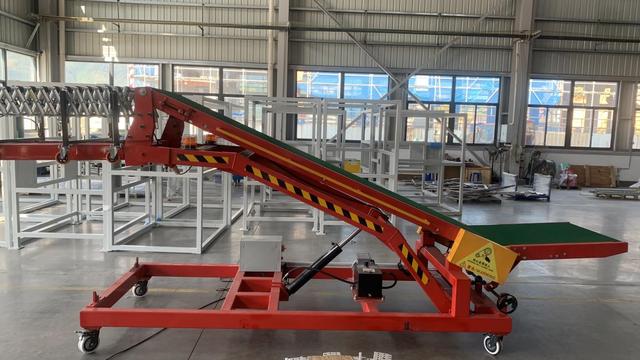
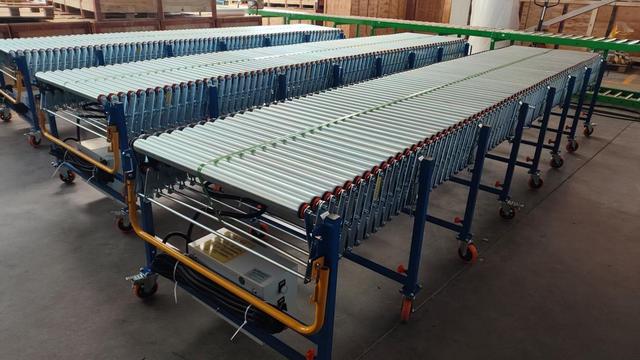
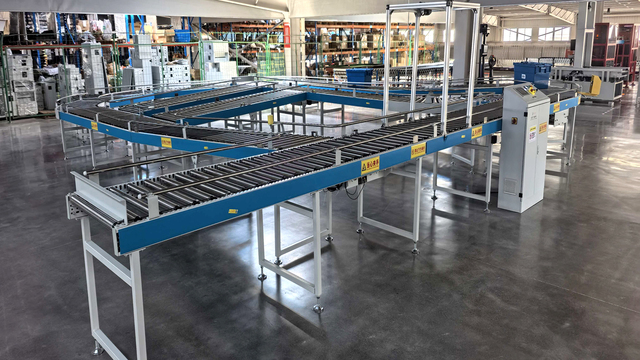
Maith Conveyor’s core product portfolio includes roller conveyor systems, belt conveyor lines, pallet handling systems, sorting conveyors, telescopic loading conveyors, gravity conveyor modules, and intelligent warehouse automation systems. By integrating PLC control systems, sensor-based tracking technology, AI-driven logistics optimization, and modular structural design, the company delivers efficient and scalable material flow solutions tailored to modern supply chain demands.
Driven by continuous innovation and smart logistics development, Hangzhou Maith Conveyor Co., Ltd. is committed to improving warehouse productivity, reducing operational costs, and enhancing automation efficiency. The company provides customized engineering solutions, flexible system integration, and reliable after-sales support, building long-term partnerships with global customers in the rapidly evolving logistics and automation industry.
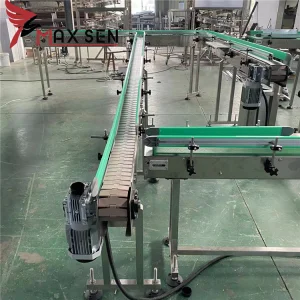
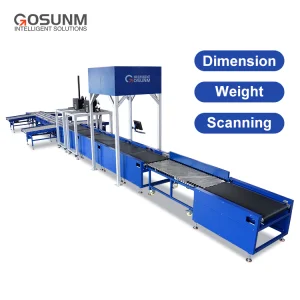

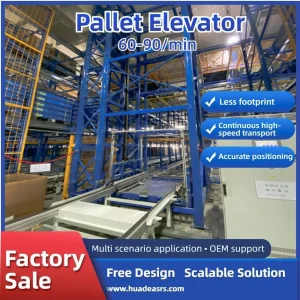
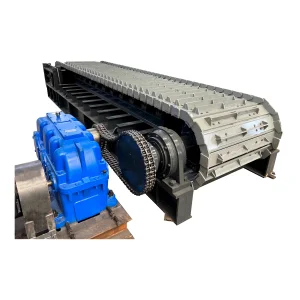
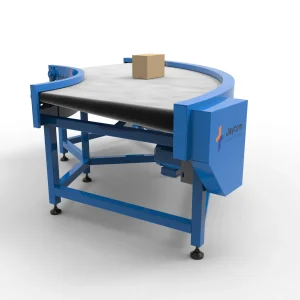
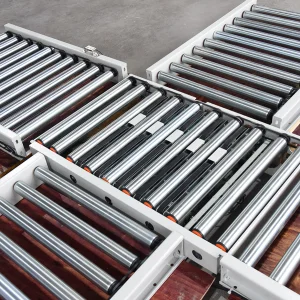
The global sanitary and industrial conveyor landscape is undergoing an unprecedented transformation driven by Industry 4.0 paradigms. Modern supply chains demand uncompromising hygiene standards, real-time telemetry, predictive maintenance, and seamless WMS (Warehouse Management System) integration. As global e-commerce volumes surge and manufacturing facilities pivot towards automated lights-out operations, conveyor systems are no longer passive transport tracks—they are active, intelligent nodes equipped with AI-driven sorting algorithms and IoT sensor arrays.
Meeting diverse industrial requirements—from pharmaceutical and food processing sanitary environments to heavy-duty mining and automated airport baggage handling—requires meticulous engineering. Hangzhou Maith Conveyor Co., Ltd. leads this domain by combining robust structural metallurgy with advanced polymer engineering, ensuring optimal corrosion resistance, minimal downtime, and maximum energy efficiency across all deployment vectors.
 Maith Conveyor