Industrial Automation Engineering Whitepaper 2025

Top China Cable Conveyor Factories & Exporters

An Executive Guide to Advanced Cable Conveyors, Smart Belt Systems, and Automated Bulk Material Handling Infrastructure Engineered in China for Global Enterprise Demand.

Smart Systems Portfolio Phase I

High-Efficiency Logistics & Material Conveyor Systems

Explore precision-engineered conveyor solutions designed for high-density warehousing, cleanroom processing, high-speed sorting, and heavy industrial applications.
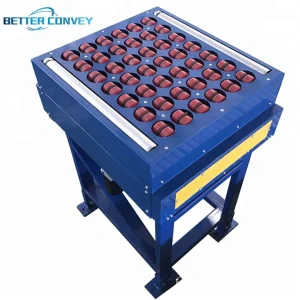
Belt Conveyor Wooden Case Warehouse Automated Parcel Line Intelligent Sorting Lines

Belt Conveyor Wooden Case Warehouse Automated Parcel Line Intelligent Sorting Lines

View System Details
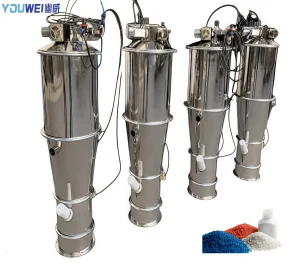
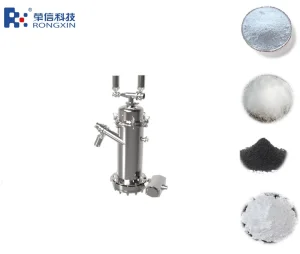
Food Grade Vacuum Conveyor Systems for Efficient Material Handling

Food Grade Vacuum Conveyor Systems for Efficient Material Handling

View System Details
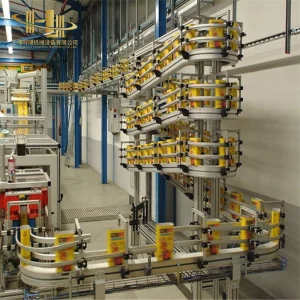
Boxed Beverage Conveyor System Suitable for Small Package Drinks Durable Hygienic Food Grade Conveyor

Boxed Beverage Conveyor System Suitable for Small Package Drinks Durable Hygienic Food Grade Conveyor

View System Details
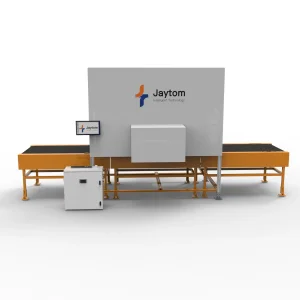
High Speed Automatic Sorting System with Dws Scan Automated Parcel for Logistics Belt Conveyor Made in China

High Speed Automatic Sorting System with Dws Scan Automated Parcel for Logistics Belt Conveyor Made in China

View System Details
Drop Forged Flight Chain Standard Series 12534 for Different Conveyor Systems

Drop Forged Flight Chain Standard Series 12534 for Different Conveyor Systems

View System Details
AI-Powered Vacuum Conveyor Self-Optimizing System with Predictive Maintenance Alerts

AI-Powered Vacuum Conveyor Self-Optimizing System with Predictive Maintenance Alerts

View System Details
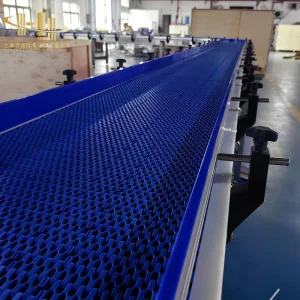
Customizable Snacks Plastic Modular Belt Conveyor Systems for Efficient Food Beverage Industrial Production Lines

Customizable Snacks Plastic Modular Belt Conveyor Systems for Efficient Food Beverage Industrial Production Lines

View System Details
Heavy-Duty Industry Powered Pallet Handling Roller Conveyor System, Pallet Chain Drive Live Roller Conveyor

Heavy-Duty Industry Powered Pallet Handling Roller Conveyor System, Pallet Chain Drive Live Roller Conveyor

View System Details
Industry Economics & Engineering Shift

The Global Evolution of Cable & Bulk Material Handling Conveyors

Analyzing the shift from legacy mechanical drag chains to high-speed cable technology, energy-efficient tubular drag systems, and integrated AI material flow solutions.

In modern industrial manufacturing and global logistics, material handling systems represent the arterial backbone of operational efficiency. As multinational enterprises face escalating labor costs, stringent environmental dust-containment regulations, and the imperative for zero product degradation, the choice of conveyor architecture has moved to center stage. Among the various continuous conveying technologies, tubular cable conveyors, specialized flight chain conveyors, and automated modular belt systems have surged in global adoption.

Cable conveyors—utilizing ultra-high-molecular-weight discs attached to a flexible, high-tensile stainless steel cable running within a sealed tube—offer unparalleled advantages in moving fragile powders, bulk solids, and delicate foodstuffs without thermal degradation or particle segregation. Concurrently, heavy-duty industrial logistics hubs demand integrated roller, pallet, and vertical lift systems to maintain continuous 24/7 warehouse throughput.

Information Gain Insights: Cable vs. Pneumatic vs. Conventional Drag Conveyors

Engineering data demonstrates that tubular cable conveyors reduce energy consumption by up to 55% to 70% compared to dense-phase pneumatic conveying systems, while keeping product friction degradation below 0.05%. Unlike open belt conveyors, tubular cable and vacuum systems guarantee 100% dust containment, fulfilling strict OSHA and ATEX explosion protection mandates.

Conveyor Technology Category Energy Efficiency (kWh/Ton) Material Degradation Rate Dust Containment Level Maintenance & Lifecycle TCO
Tubular Cable Conveyor System Ultra-Low (1.5 - 3.0 kW) Near Zero (< 0.05%) 100% Fully Hermetic Seal Low (Modular Cable & Disc Replace)
Dense-Phase Pneumatic System High (15.0 - 30.0 kW) Moderate to High (At bends) 100% Fully Hermetic Seal High (Compressor & Valve Wear)
Heavy Drop-Forged Chain Conveyor Moderate (5.5 - 11.0 kW) Low to Moderate Partial (Enclosed Casing) Medium (Heavy Duty Sprocket Wear)
Standard Open Belt / Roller Lines Low (2.2 - 5.5 kW) Low Unsealed (Requires External Hoods) Low to Medium (Belt Tensioning)

Low Power Footprint

Operates using low-horsepower drive motors (typically 2 to 7.5 HP), drastically slashing monthly kilowatt-hour consumption compared to high-pressure blowers.

Gentle Handling & Zero Dust

Material is gently swept along the sealed tube by smooth polymer discs, preventing fragile friable items like coffee beans, pet food, and coated pills from breaking.

Flexible Multi-Plane Routing

Able to route through complex 3D plant spaces—including vertical ascents, tight angles, and multi-inlet/outlet discharge pathways without transfer points.

E-E-A-T Verified Manufacturer Focus

China's Premier Cable Conveyor & Smart Logistics Factory Hub

Discover how Hangzhou Maith Conveyor Co., Ltd. combines advanced European-standard design with precision Chinese manufacturing efficiency to power enterprise logistics global supply chains.

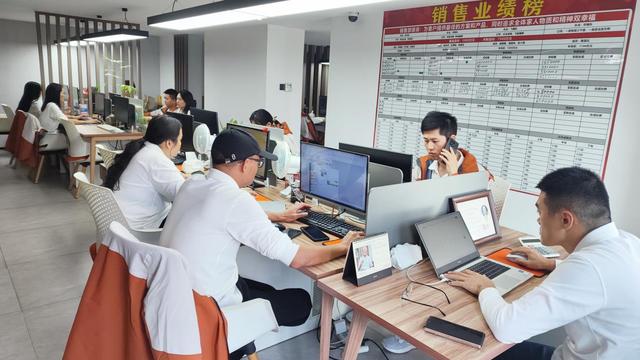
Hangzhou Maith Conveyor Co., Ltd. is a professional manufacturer specializing in warehouse conveyor systems, smart logistics automation equipment, and advanced material handling solutions for global distribution, manufacturing, and e-commerce industries. Established in 2013 and headquartered in Hangzhou, China, the company integrates research and development, system design, precision manufacturing, installation services, and international OEM/ODM support into a complete industrial automation ecosystem.

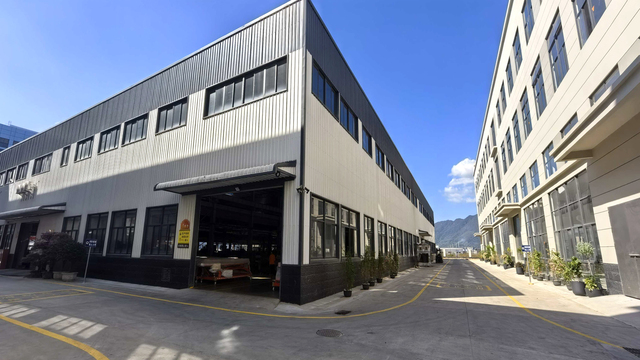
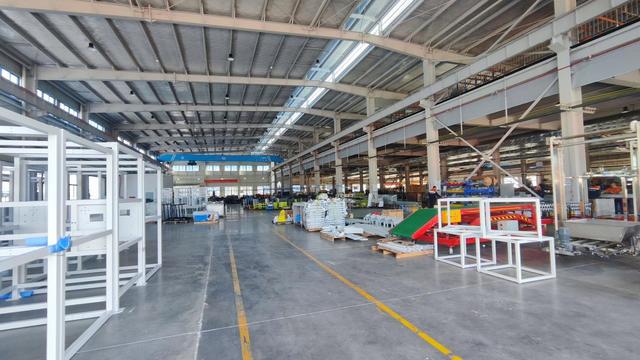
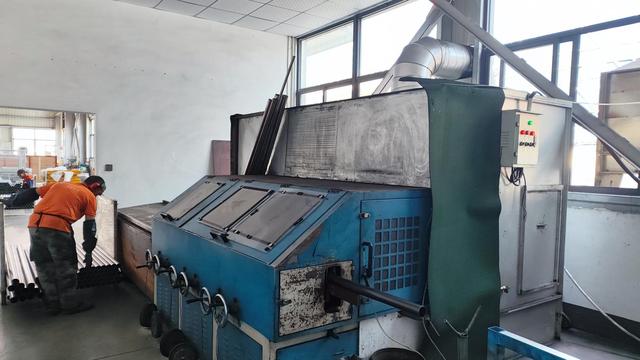
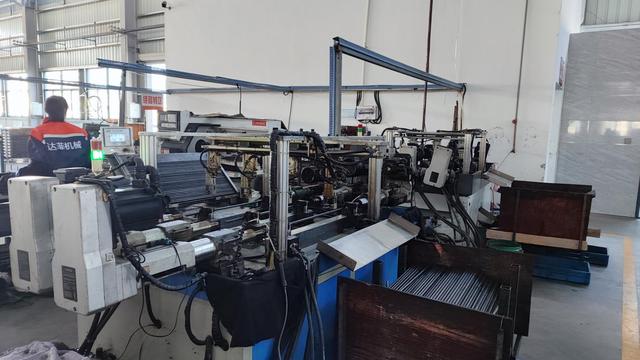
The company operates a modern production base covering approximately 30,000 square meters with more than 360 employees, including mechanical engineers, automation specialists, and software control experts. Equipped with advanced fabrication workshops, automated assembly lines, and rigorous quality inspection systems, Maith Conveyor ensures high performance, stability, and durability across all conveyor solutions. Annual production capacity exceeds 6,500 complete conveyor systems, serving clients in warehousing, logistics centers, airports, retail distribution hubs, manufacturing plants, and fulfillment operations worldwide.

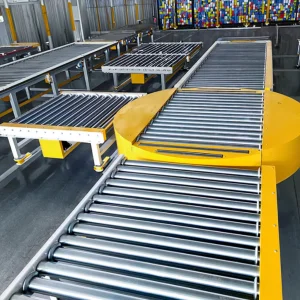
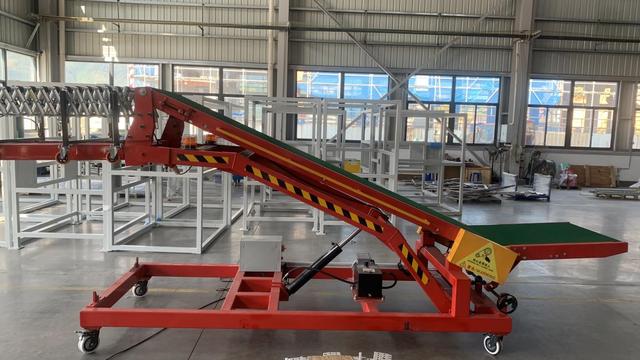
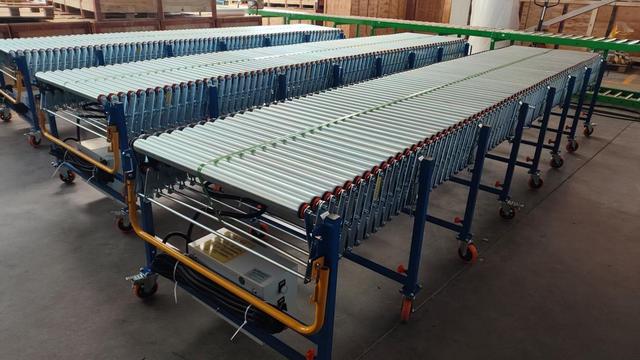
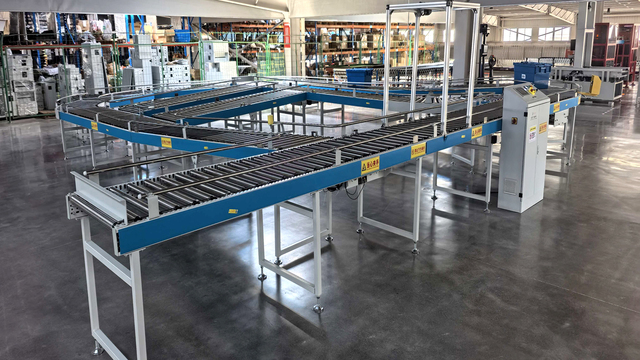
Maith Conveyor’s core product portfolio includes roller conveyor systems, belt conveyor lines, pallet handling systems, sorting conveyors, telescopic loading conveyors, gravity conveyor modules, and intelligent warehouse automation systems. By integrating PLC control systems, sensor-based tracking technology, AI-driven logistics optimization, and modular structural design, the company delivers efficient and scalable material flow solutions tailored to modern supply chain demands.

Driven by continuous innovation and smart logistics development, Hangzhou Maith Conveyor Co., Ltd. is committed to improving warehouse productivity, reducing operational costs, and enhancing automation efficiency. The company provides customized engineering solutions, flexible system integration, and reliable after-sales support, building long-term partnerships with global customers in the rapidly evolving logistics and automation industry.
30,000 m²
Modern Production Base
360+
Engineers & Staff
6,500+
Annual Systems Capacity
10+ Years
Global OEM/ODM Expertise

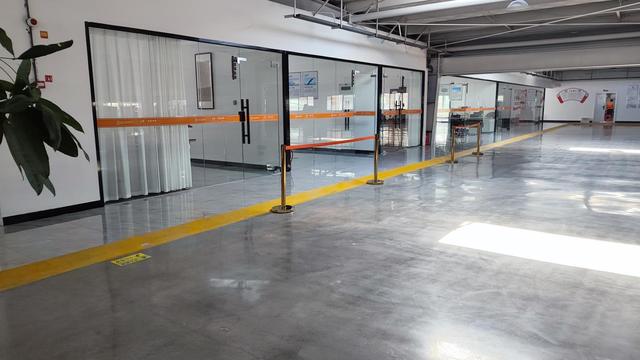
Manufacturing Workshop & Rigorous Inspection Facilities

Industry Solutions Architecture

Localized Applications & Global Enterprise Procurement Needs

From cleanroom food processing to high-velocity e-commerce sorting and heavy bulk material transfers, explore targeted application profiles.

Food & Beverage Processing

Utilizing FDA-compliant UHMW-PE flights, 316L stainless steel tubing, and CIP (Clean-in-Place) automated washing loops. Ideal for breakfast cereals, coffee beans, nuts, and infant formula.

E-Commerce & Smart Logistics Hubs

Integrating high-speed DWS (Dimensioning, Weighing, Scanning) stations with intelligent belt and parcel sorting modules capable of processing up to 12,000 parcels per hour.

Chemical & Powder Manufacturing

Dust-tight tubular cable designs eliminate explosive ambient dust buildup, fulfilling European ATEX zone specifications for fine carbon black, titanium dioxide, and specialty resins.

Global Procurement Checklist: Key Criteria for Selecting Chinese Cable Conveyor Exporters

When sourcing custom material handling systems from Chinese manufacturers, procurement directors must evaluate vendors across five vital technological vectors:

  • Cable Integrity & Tensile Load Specs: Ensure cables utilize 316 grade stainless steel with high-flex strand geometry (e.g., 7x19 construction) and specialized nylon/polyurethane encapsulation to prevent fraying and stretch over long duty cycles.
  • Disc-to-Cable Dynamic Attachment: Inspect the attachment mechanical locking system. Swaged stainless steel connectors ensure discs remain permanently fixed at precise intervals without slippage under high torque loads.
  • Control System Interoperability: Require industrial PLC integration (Siemens S7-1500, Allen-Bradley CompactLogix) with native Ethernet/IP, PROFINET, or Modbus TCP protocols for seamless SCADA connection.
  • AI & Predictive Maintenance Sensor Suites: Modern lines must feature digital thermal monitoring on bearing housings, vibration analysis transducers, and optical disc counters for automated wear warnings.
  • Factory Acceptance Testing (FAT) Protocols: Ensure the exporter provides full-load pre-shipment dry runs and digital twin simulation reports before containerized export.
Heavy Industrial & Warehouse Automation Phase II

Advanced Conveyor Systems & Heavy-Duty Machinery

Explore specialized industrial machinery, stackers, electric motorized roller systems, and modular pallet transport solutions engineered for continuous global operation.
Customized Automatic Packing Line Roller Electric Belt Pallet Conveyor System

Customized Automatic Packing Line Roller Electric Belt Pallet Conveyor System

View System Details
Premium Chain Conveyor System Adjustable Motorized Conveyor System for Pallet Warehouse System

Premium Chain Conveyor System Adjustable Motorized Conveyor System for Pallet Warehouse System

View System Details
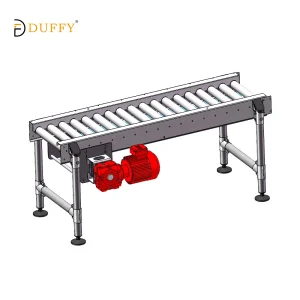
Electric Powered Roller Conveyor System for Automated Logistics Sorting Lines

Electric Powered Roller Conveyor System for Automated Logistics Sorting Lines

View System Details
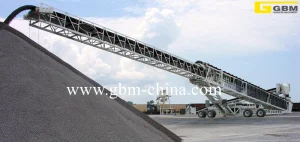
Shiploader Telescopic Stacker Conveyor System for Bulk Cargo Handling

Shiploader Telescopic Stacker Conveyor System for Bulk Cargo Handling

View System Details
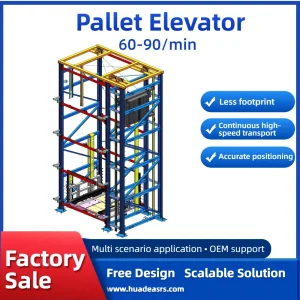
Warehouse Pallet Vertical Lift Conveyors System for Heavy and Buly Loads

Warehouse Pallet Vertical Lift Conveyors System for Heavy and Buly Loads

View System Details
Customized PVC Belt Conveyor System for Furniture Production Line

Customized PVC Belt Conveyor System for Furniture Production Line

View System Details
Carton Box Driven Roll Conveyor Portable Gravity Roller Conveyor System for Flexible Workshop Application

Carton Box Driven Roll Conveyor Portable Gravity Roller Conveyor System for Flexible Workshop Application

View System Details
Galvanized Steel Roller Conveyor for E Commerce Warehouse 8m to 50m Length Modular Design

Galvanized Steel Roller Conveyor for E Commerce Warehouse 8m to 50m Length Modular Design

View System Details
Future Technological Horizon

Emerging Trends: AI-Driven Conveying & Industry 4.0 Integration

How Chinese manufacturers are pioneering smart conveyor systems with automated tensioning, self-healing diagnostics, and IoT cloud platforms.

AI Predictive Maintenance

Integrated vibration and temperature sensors monitor drive gearboxes and cable tensioners continuously. AI algorithms forecast mechanical wear up to 30 days prior to component failure.

Automated Cable Tensioning

Pneumatic and motorized dynamic tension units auto-adjust cable slack caused by thermal expansion, ensuring constant velocity and preventing disc jams inside elbow sections.

Modular Architecture

Standardized flange-connected tubular segments and quick-release access hatches allow rapid layout reconfigurations and quick installation turnaround for expanding facilities.

Technical Clarifications & Buying Intent

Frequently Asked Questions (FAQ)

In-depth responses to core engineering and procurement queries regarding China-manufactured cable conveyors and automated logistics lines.

What is the primary difference between a tubular cable conveyor and a chain conveyor system?
Tubular cable conveyors utilize a high-tensile, flexible stainless steel cable encapsulated in nylon or polyurethane, running centered through a smooth tube with circular discs. This design minimizes material degradation, eliminates mechanical pin wear, operates with significantly less power, and maintains a sealed dust-tight environment. Chain conveyors (such as drop-forged flight chains) rely on heavy mechanical links suited for extreme bulk loads, high-temperature bottom-ash, or aggressive mining rocks where absolute ultimate tensile resistance supersedes delicate material handling.
How does Hangzhou Maith Conveyor Co., Ltd. ensure international quality compliance?
Hangzhou Maith Conveyor Co., Ltd. enforces rigorous quality inspection standards across its 30,000 square meter factory. Every system undergoes laser-alignment inspection, structural stress testing, dynamic balancing, and electrical safety checks under full load simulations. All systems exported to Europe and North America comply with CE marking, ISO 9001 certification, and optional ATEX / FDA food-grade material standards depending on destination requirements.
Can cable conveyor systems handle fragile or moisture-sensitive bulk materials?
Yes. Cable conveyors are specifically recognized worldwide as the gentlest continuous handling medium for fragile products such as roasted coffee beans, freeze-dried powders, extruded pet food kibble, and snack foods. The solid polymer discs move smoothly within the sealed tube, gently pushing product pockets without high-velocity air agitation or drop impacts that cause breakage or particle separation.
What engineering information is required to get an accurate OEM factory quote?
To provide an engineered quote, our technical team requires: (1) Material characteristics including bulk density, particle size, moisture level, and temperature; (2) Conveying rate in cubic meters or metric tons per hour; (3) Spatial layout dimensions showing vertical lift distance, horizontal run length, and number of bends; and (4) Electrical voltage and preferred control ecosystem (e.g., Siemens PLC, Schneider electrics).
How are AI-driven features implemented into vacuum and belt conveyor systems?
AI-enabled conveyor systems utilize smart sensor networks connected to an edge PLC. Sensors track motor vibration spectrums, current draw spikes, belt misalignments, filter pressure drops (on vacuum conveyors), and bearing thermal trends. Edge AI processes these signals to optimize speed dynamically, initiate auto-cleaning pulse cycles, and issue predictive maintenance alerts via cloud dashboards before minor wear causes unplanned line downtime.