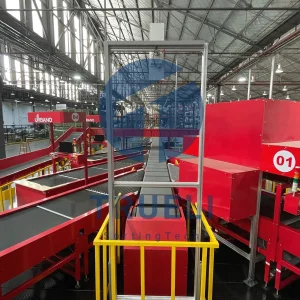
Explore our cutting-edge manufacturing lines designed for high-efficiency industrial processing and smart warehousing ecosystems.


Anchored in Hangzhou, China, Hangzhou Maith Conveyor Co., Ltd. represents the peak of engineering excellence in global logistics and custom OEM vacuum conveying architecture.
Hangzhou Maith Conveyor Co., Ltd. is a professional manufacturer specializing in warehouse conveyor systems, smart logistics automation equipment, and advanced material handling solutions for global distribution, manufacturing, and e-commerce industries. Established in 2013 and headquartered in Hangzhou, China, the company integrates research and development, system design, precision manufacturing, installation services, and international OEM/ODM support into a complete industrial automation ecosystem.
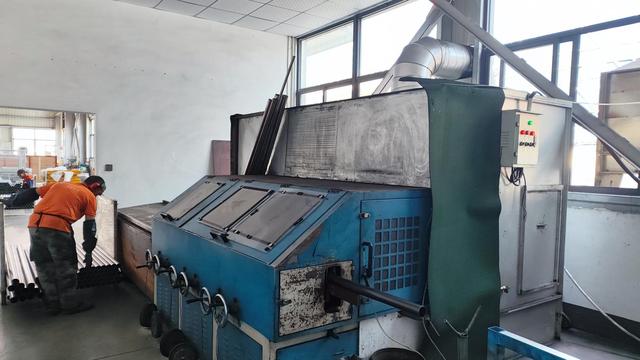
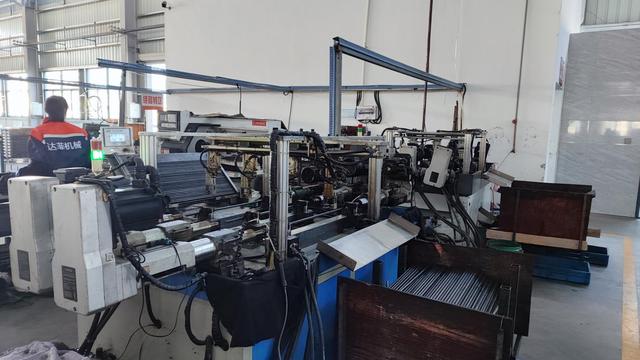
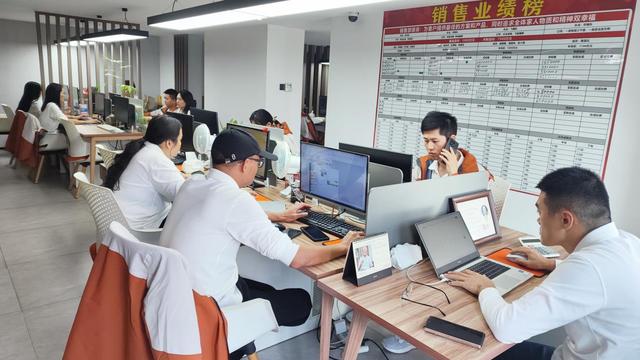
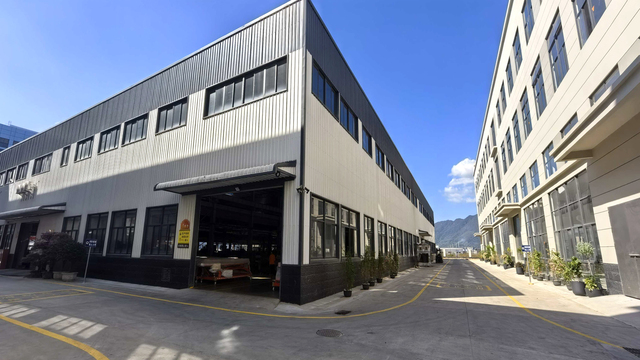
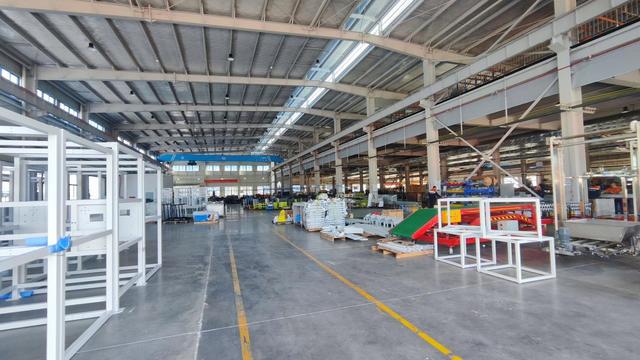
The company operates a modern production base covering approximately 30,000 square meters with more than 360 employees, including mechanical engineers, automation specialists, and software control experts. Equipped with advanced fabrication workshops, automated assembly lines, and rigorous quality inspection systems, Maith Conveyor ensures high performance, stability, and durability across all conveyor solutions.
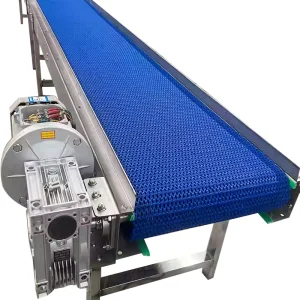
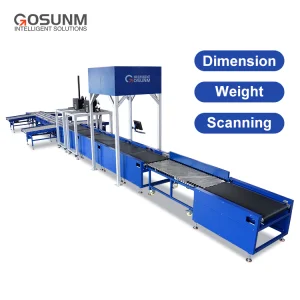
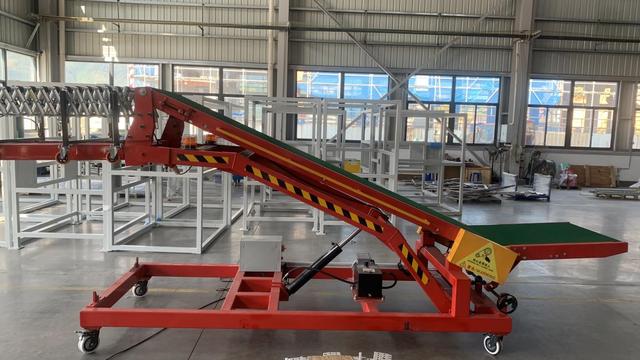
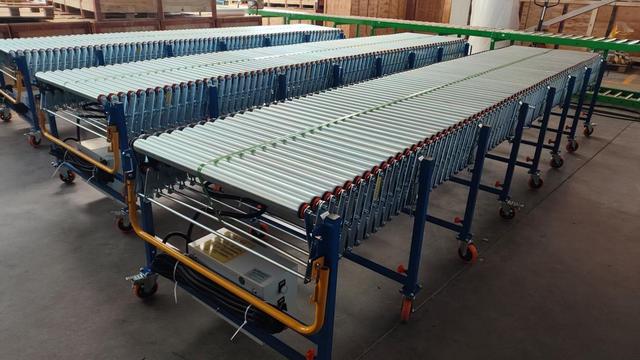
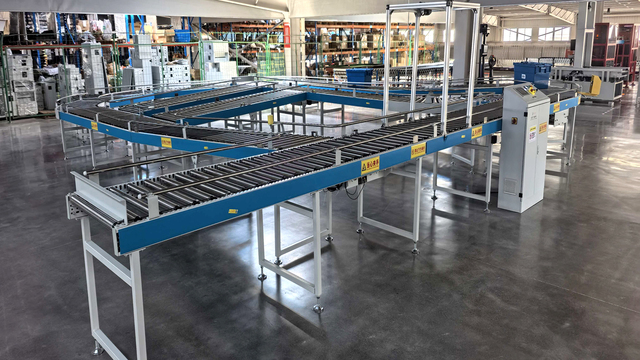
Annual production capacity exceeds 6,500 complete conveyor systems, serving clients in warehousing, logistics centers, airports, retail distribution hubs, manufacturing plants, and fulfillment operations worldwide. Maith Conveyor’s core product portfolio includes roller conveyor systems, belt conveyor lines, pallet handling systems, sorting conveyors, telescopic loading conveyors, gravity conveyor modules, and intelligent warehouse automation systems.
By integrating PLC control systems, sensor-based tracking technology, AI-driven logistics optimization, and modular structural design, the company delivers efficient and scalable material flow solutions tailored to modern supply chain demands. Driven by continuous innovation and smart logistics development, Hangzhou Maith Conveyor Co., Ltd. is committed to improving warehouse productivity, reducing operational costs, and enhancing automation efficiency. The company provides customized engineering solutions, flexible system integration, and reliable after-sales support, building long-term partnerships with global customers in the rapidly evolving logistics and automation industry.
Navigating the next generation of pneumatic transport systems through deep IoT integration and energy-efficient fluid dynamics.
Our research and development pipeline focuses on optimizing gas-solid two-phase flow simulations. By utilizing advanced computational fluid dynamics (CFD), our custom vacuum conveyor factories engineer low-velocity, high-concentration conveying systems that drastically reduce particle degradation and pipe wear for fragile pharmaceutical and chemical powders.
Future iterations of our vacuum conveyors incorporate edge-computing microcontrollers, such as ESP32 and ARM-based processors, embedded directly into filter cleaning cycles and vacuum pump assemblies. Real-time telemetry tracks pressure differentials, filter saturation, and volumetric flow rates, enabling predictive maintenance protocols.
With global carbon reduction mandates tightening, our engineering teams have developed variable frequency drive (VFD) controlled Roots blowers and multi-stage Venturi vacuum generators that dynamically adjust suction power based on real-time material load, cutting electrical consumption by up to 35%.
Tailored engineering frameworks designed to meet stringent global standards across pharmaceutical, chemical, and food processing verticals.
From airtight containment systems for toxic active pharmaceutical ingredients (APIs) to explosion-proof (ATEX-certified) vacuum conveyors for combustible carbon and metal powders, Maith Conveyor delivers turn-key execution. Our modular configurations allow seamless integration with blending machines, tablet presses, and automated packaging lines.
Operating as a premier exporter, we ensure complete compliance with international regulatory frameworks including CE, ISO9001, FDA food-grade material standards, and UL electrical specifications. Our localization support includes regional engineering consultations, spare parts warehousing, and multilingual remote diagnostic assistance.
Leveraging intelligent manufacturing clusters to deliver unmatched cost-to-performance ratios without compromising precision.
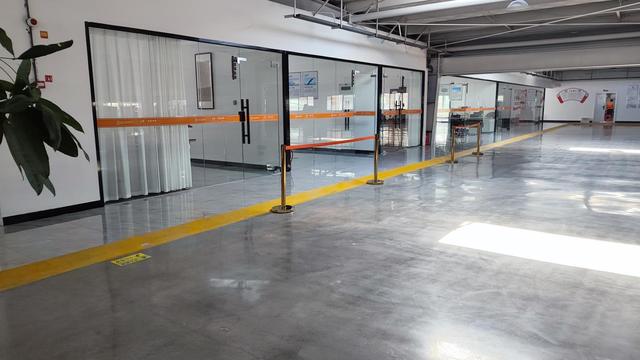
Advanced Production Facility
Annual System Output Capacity
Engineers & Specialized Technicians
By housing laser cutting, CNC robotic welding, surface passivation treatment, and automated electrical panel assembly under one roof, Maith Conveyor insulates global procurement partners from supply chain volatility. Our stringent Quality Assurance (QA) protocol involves 100% pre-shipment dry runs and pressure-leak testing for every custom vacuum conveyor system.
Addressing core technical and logistical inquiries for international project managers and plant engineers.
A: Vacuum conveyors operate in a completely sealed, enclosed pipeline utilizing negative pressure. This eliminates dust leakage, prevents environmental cross-contamination, protects operators from hazardous or toxic substances, and minimizes mechanical product degradation during transit.
A: Yes. We offer specialized configurations featuring 316L stainless steel contact surfaces, anti-static food-grade hoses, inert gas purging systems, and ATEX/Ex-proof certified electrical components suitable for hazardous chemical and pharmaceutical environments.
A: Standard modular systems typically ship within 3 to 4 weeks. Fully customized, multi-station engineering projects involving complex PLC integration and bespoke piping layouts generally require 6 to 8 weeks from design approval to factory dispatch.
A: We provide comprehensive 3D installation drawings, step-by-step video configuration guides, and remote IoT diagnostics. For large-scale integration projects, our experienced automation engineers are available for on-site commissioning and operator training worldwide.
Discover additional high-durability conveying modules engineered to complete your automated factory infrastructure.

 Maith Conveyor