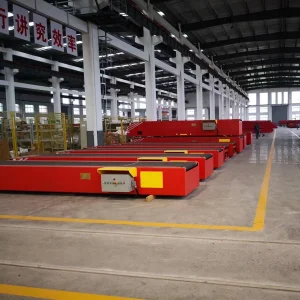
Engineered for high-efficiency loading, unloading, and distribution operations in Bouaké logistics hubs.
Comprehensive analysis of industrial modernization, supply chain efficiency, and automated material handling infrastructure in Bouaké.
Bouaké, serving as a critical commercial and transportation nexus, plays a pivotal role in regional trade, agricultural distribution, and light manufacturing within West Africa. As commercial activities expand rapidly, local warehouses, distribution centers, and fulfillment hubs face unprecedented pressure to upgrade their material handling capabilities. Traditional manual loading and unloading methods are increasingly bottlenecking supply chain throughput, leading to higher labor costs and prolonged turnaround times for commercial trucks.
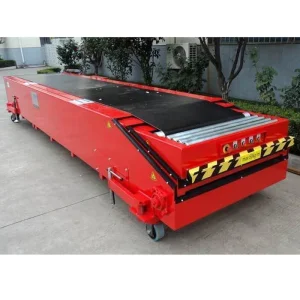
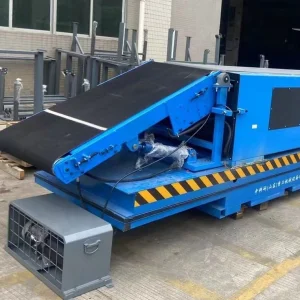
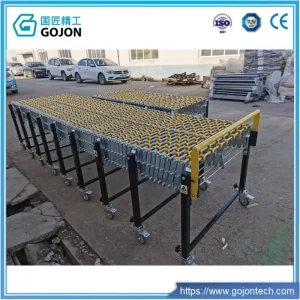
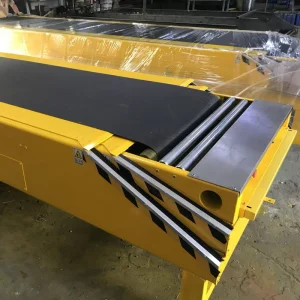
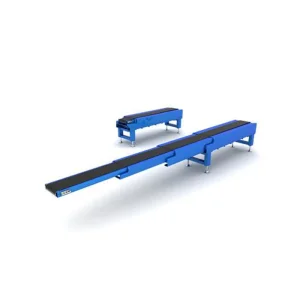
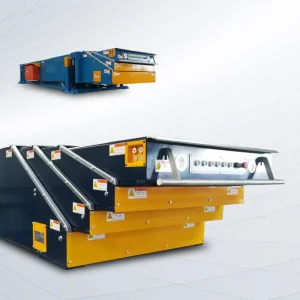
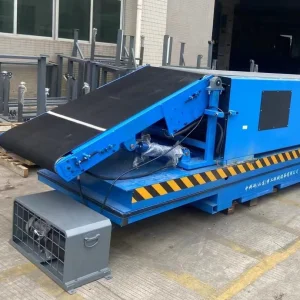
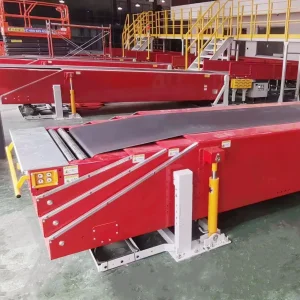
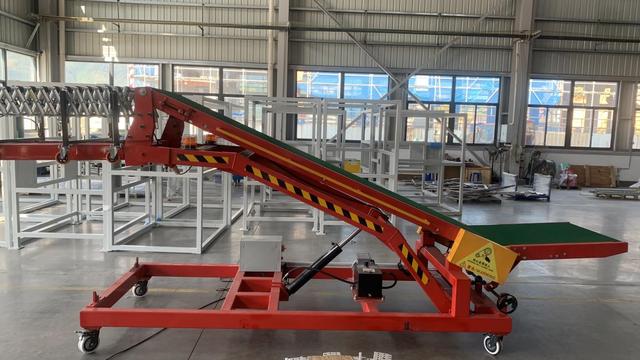
To bridge this efficiency gap, industrial facilities across Bouaké are rapidly adopting automated material flow technologies. The integration of a high-performance Telescopic Conveyor System allows warehouses to minimize worker fatigue, accelerate truck loading cycles by up to 50%, and protect fragile parcels and bulk goods from transit damage. As a trusted supplier and manufacturing partner, Hangzhou Maith Conveyor Co., Ltd. delivers customized, heavy-duty telescopic systems specifically engineered to withstand rigorous operational environments while maximizing uptime.
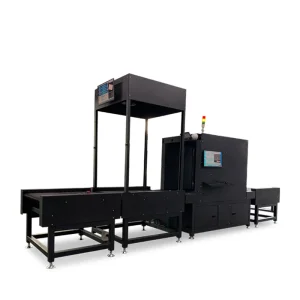
The global logistics automation market is undergoing a seismic shift driven by IoT integration, AI-driven sorting algorithms, and modular design principles. In emerging commercial markets like Bouaké, flexibility and scalability are paramount. Modern telescopic conveyors are no longer simple mechanical extension belts; they are intelligent nodes integrated directly into Warehouse Management Systems (WMS) and Dimensioning, Weighing, and Scanning (DWS) networks.
Key technological advancements include variable frequency speed control, bidirectional belt movement, collision-avoidance sensors, and energy-efficient electric drives. These features empower warehouse operators in Bouaké to seamlessly scale their operations during peak seasonal demands without making massive infrastructure overhauls. Maith Conveyor remains at the forefront of this evolution, incorporating cutting-edge PLC controls and durable stainless steel construction into every production line.
Global enterprises and regional distributors demand robust, fail-safe, and low-maintenance automation equipment. Supply chain managers prioritize suppliers who can offer end-to-end solutions—from initial layout design and CAD modeling to precision manufacturing, international shipping, and remote technical commissioning.
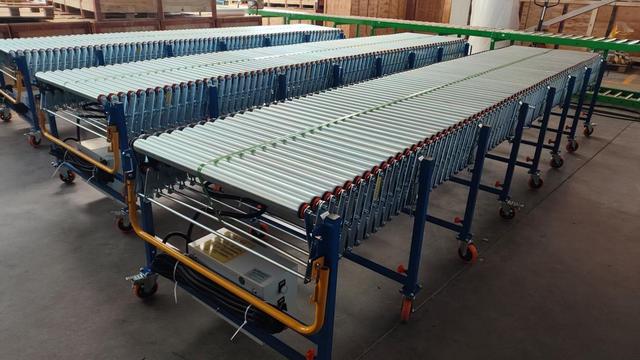
Hangzhou Maith Conveyor Co., Ltd. fulfills these macro requirements through its comprehensive industrial automation ecosystem. Operating from a 30,000-square-meter facility with over 360 skilled professionals, the company ensures strict compliance with international quality standards. Whether supplying extendable belt conveyors for e-commerce parcel sorting or heavy-duty telescopic stackers for bulk cargo handling, Maith provides bespoke engineering solutions designed to optimize total cost of ownership (TCO) for international buyers.
Deploying advanced automation equipment internationally requires rigorous local support frameworks and strict regulatory compliance. Maith Conveyor provides comprehensive documentation, video installation guides, modular plug-and-play wiring, and responsive after-sales engineering support to ensure seamless integration in Bouaké facilities.
Looking toward the future, our technical roadmap emphasizes green manufacturing, solar-ready energy conservation models, and predictive maintenance enabled by IoT diagnostics. By maintaining rigorous CE, ISO, and safety certifications, we guarantee that every telescopic conveyor system delivered to the Bouaké market meets the highest benchmarks of reliability, operator safety, and operational excellence.
Hangzhou Maith Conveyor Co., Ltd. is a professional manufacturer specializing in warehouse conveyor systems, smart logistics automation equipment, and advanced material handling solutions for global distribution, manufacturing, and e-commerce industries. Established in 2013 and headquartered in Hangzhou, China, the company integrates research and development, system design, precision manufacturing, installation services, and international OEM/ODM support into a complete industrial automation ecosystem.
The company operates a modern production base covering approximately 30,000 square meters with more than 360 employees, including mechanical engineers, automation specialists, and software control experts. Equipped with advanced fabrication workshops, automated assembly lines, and rigorous quality inspection systems, Maith Conveyor ensures high performance, stability, and durability across all conveyor solutions. Annual production capacity exceeds 6,500 complete conveyor systems, serving clients in warehousing, logistics centers, airports, retail distribution hubs, manufacturing plants, and fulfillment operations worldwide.
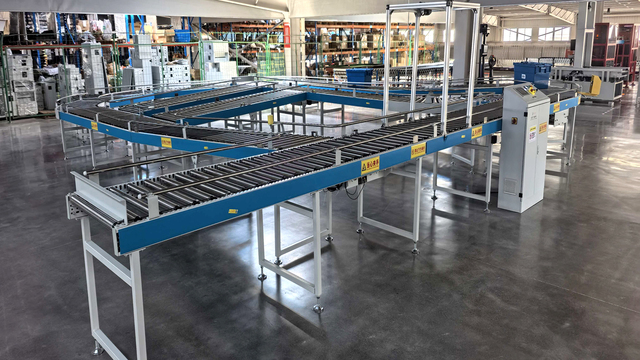
Maith Conveyor’s core product portfolio includes roller conveyor systems, belt conveyor lines, pallet handling systems, sorting conveyors, telescopic loading conveyors, gravity conveyor modules, and intelligent warehouse automation systems. By integrating PLC control systems, sensor-based tracking technology, AI-driven logistics optimization, and modular structural design, the company delivers efficient and scalable material flow solutions tailored to modern supply chain demands.
Driven by continuous innovation and smart logistics development, Hangzhou Maith Conveyor Co., Ltd. is committed to improving warehouse productivity, reducing operational costs, and enhancing automation efficiency. The company provides customized engineering solutions, flexible system integration, and reliable after-sales support, building long-term partnerships with global customers in the rapidly evolving logistics and automation industry.
Partner with Hangzhou Maith Conveyor Co., Ltd. for state-of-the-art telescopic conveyor solutions.
Send Inquiry NowExplore our extensive range of certified material handling systems designed for global industrial applications.
 Maith Conveyor