Explore our foundational smart automated handling lines deployed globally across high-volume distribution centers, processing hubs, and precision assembly lines.
The industrial and commercial landscape serving Santana—ranging from its strategic port facilities, regional distribution centers, agricultural processing nodes, and emerging assembly operations—is undergoing a rapid technological migration toward autonomous logistics. Situated as a vital conduit for multimodal freight, raw material processing, and localized consumer distribution, enterprises operating in and around Santana face distinct operational demands that legacy mechanical conveyors can no longer satisfy.
Industrial facilities in Santana encounter severe environmental and operational challenges: high ambient humidity, micro-dust contamination from bulk cargo operations, fluctuations in regional power grids, and an increasing shortage of specialized manual labor. Traditional material handling systems fail under these conditions due to belt mistracking, roller bearing burnout, unpredicted motor stalls, and rigid throughput bottlenecks during peak seasonal demand.
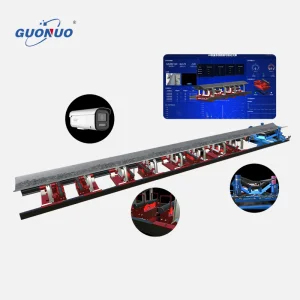
Integrating dynamic AI belt scale systems and heavy-duty stainless steel transport lines capable of continuous 8,000 t/h bulk handling directly synchronized with Santana port loading terminals.
Sanitary, IP69K-rated, self-cleaning vacuum conveyors and precision automated food delivery networks engineered to maintain absolute compliance with international food safety standards.
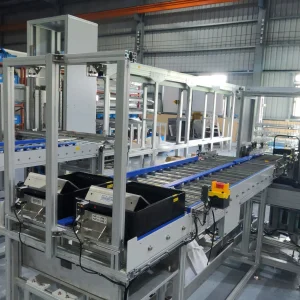
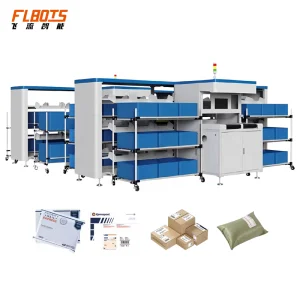
High-speed 3D vision putwalls and automated steerable wheel sorters operating at 2.5 m/s to eliminate mis-sorts across regional fulfillment centers serving Santana consumer markets.
Modern AI-controlled conveyor automation systems represent a quantum leap over conventional Programmable Logic Controller (PLC)-only architecture. By fusing embedded edge computing boards, machine vision neural networks, and real-time sensor feedback loops, our systems transform passive kinetic steel into intelligent, adaptive transport networks.
Utilizing high-frame-rate industrial PCBA vision processing boards paired with 3D depth cameras and multi-spectrum barcoding scanners, our dynamic sorting conveyors analyze parcel geometry, weight distribution, surface integrity, and linear velocity in under 12 milliseconds. The deep-learning neural network automatically compensates for torn labels, warped packaging, or irregular object shapes, directing steerable wheel sorters or high-speed pushers with sub-millimeter positioning accuracy.
Unplanned operational downtime in Santana production facilities costs thousands of dollars per hour. Our AI conveyor networks integrate tri-axial vibration sensors, thermal infrared monitoring arrays, and acoustic ultrasonic transducers directly onto motor gearboxes and bearing blocks. Machine learning models continuously compute Remaining Useful Life (RUL) metrics, flagging wear patterns weeks before catastrophic component failure occurs.
Rather than running motors at static maximum RPMs regardless of payload density, intelligent Variable Frequency Drives (VFDs) dynamically scale motor torque and linear velocity according to real-time volume sensors. During lull periods, sections automatically transition to ultra-low-power idle modes, cutting enterprise electrical consumption across Santana plants by up to 45% annually.
Hangzhou Maith Conveyor Co., Ltd. is a premier global manufacturer specializing in advanced warehouse conveyor systems, smart logistics automation equipment, and high-precision material handling solutions for global distribution, heavy manufacturing, battery cell production, and e-commerce industries. Established in 2013 and headquartered in Hangzhou, China, the company integrates end-to-end R&D, structural design, robotic fabrication, intelligent control software, and worldwide installation support into a cohesive automation ecosystem serving key regional markets including Santana.
Our state-of-the-art production complex spans approximately 30,000 square meters, staffed by a dedicated workforce of over 360 elite professionals—including mechanical design engineers, AI control specialists, PLC system architects, and global field technicians. With an annual capacity exceeding 6,500 complete conveyor systems, Maith Conveyor delivers unmatched supply chain agility, cost structural advantages, and continuous technological innovation.
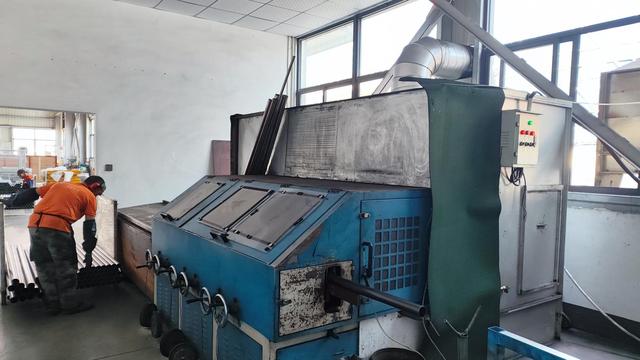
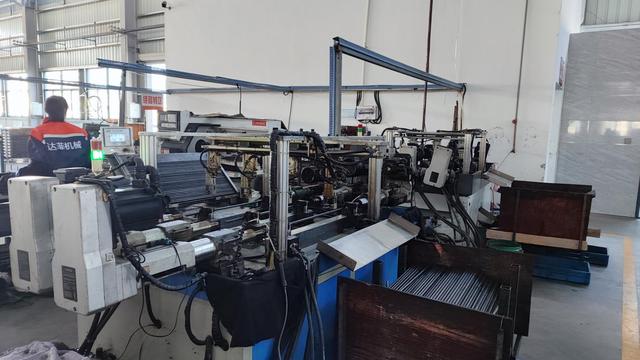
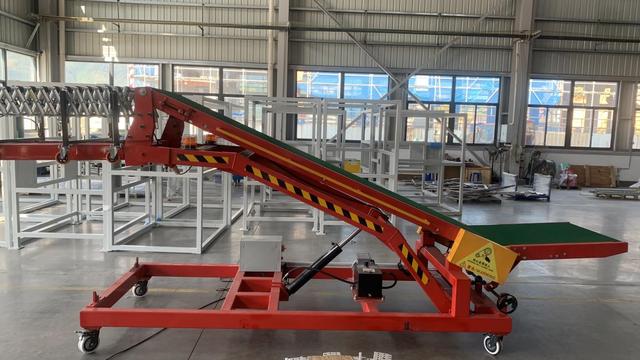
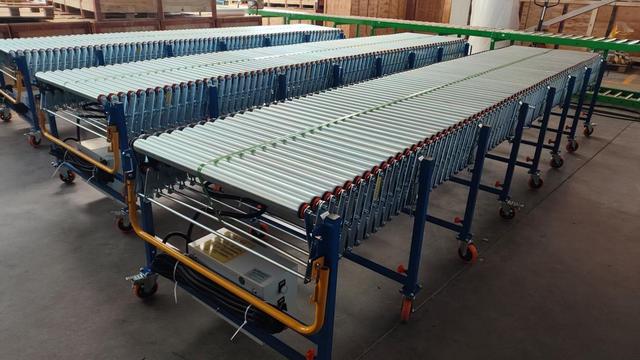
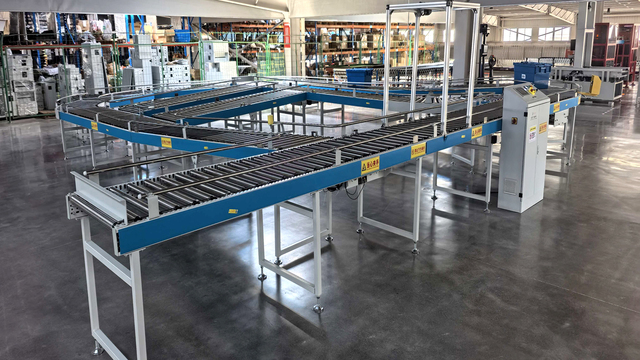
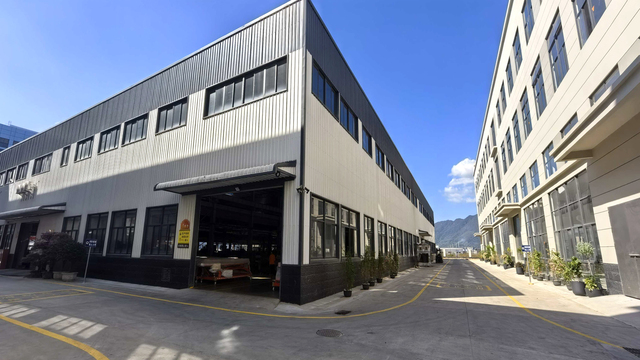
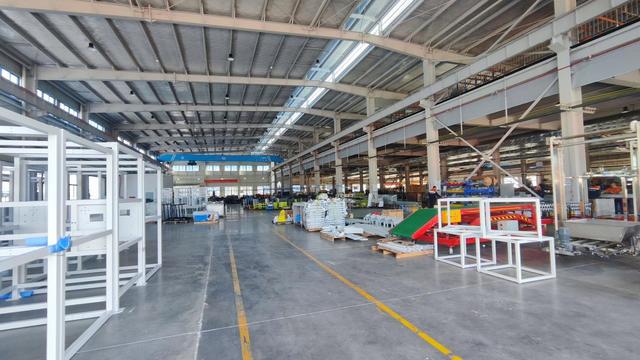
Engineered to adapt to the unique economic drivers of Santana, our customized AI conveyor systems solve sector-specific production and material flow bottlenecks.
Constructed with high-load stainless steel frames, self-lubricating dust-free rollers, and precision vertical lifts, ensuring zero particulate contamination during lithium-ion battery cell handling in automated Santana plants.
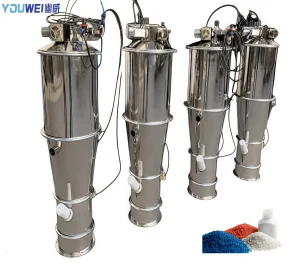
Eliminate dust emissions during pharmaceutical, chemical, or agricultural grain transfers. Our AI vacuum conveyors feature self-learning pressure-differential sensors that dynamically optimize pneumatic pulse filter cleaning cycles.
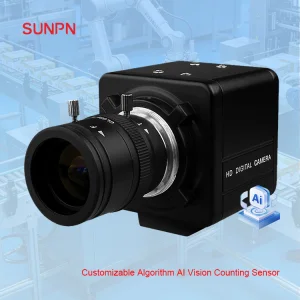
Custom AI vision recognition software integrated directly over high-speed belt lines. Cameras classify plastics, metals, paper, and industrial waste by material composition, driving high-speed air-jet sorters with 98.5% purity.
As industrial automation shifts from isolated mechanized systems to fully autonomous factory ecosystems, Hangzhou Maith Conveyor Co., Ltd. is pioneering breakthrough technologies to ensure Santana operators remain ahead of global competition.
Real-time 3D telemetry mirroring physical conveyor networks in cloud-based Digital Twins, allowing Santana plant engineers to simulate layout reconfigurations, run stress tests, and optimize flow speeds virtually before physical implementation.
Seamless protocol handshakes between fixed AI conveyor lines and Autonomous Mobile Robots (AMRs). AI orchestrators dynamically route payloads between conveyors and mobile AGVs depending on real-time line congestion.
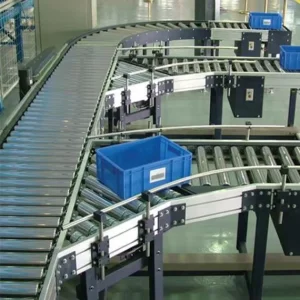
Modular roller segments with redundant driver cards. If a roller drive fails, adjacent AI roller modules instantly adjust speed and vector angles to bridge the gap, preventing line halts until scheduled maintenance.
Partnering with Hangzhou Maith Conveyor Co., Ltd. provides Santana operations with the ultimate competitive advantage: China's unparalleled industrial supply chain scale combined with rigorous international quality standards.
Every system dispatched to Santana undergoes exhaustive pre-shipment operational validation. Our manufacturing workflows strictly adhere to ISO9001:2015 Quality Management Systems, CE Machinery Directives (2006/42/EC), and UL electrical compliance guidelines. Critical mechanical components utilize premium stainless steels (304/316) and self-lubricating alloy rollers designed for 50,000+ continuous operating hours.
Thanks to standardized modular engineering, standard conveyor modules can be fabricated, tested, and containerized for shipment to Santana within 15–20 business days. We provide remote 24/7 AI telemetry diagnostics, augmented reality (AR) installation support, and on-site field engineering dispatch for comprehensive system integration.
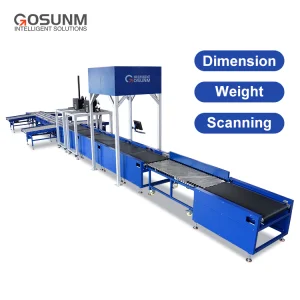
Browse our extensive selection of intelligent material transport, automated weighing, vision-based sorting, and food-grade conveying solutions.
Expert insights regarding implementation, ROI, software connectivity, and mechanical customization for Santana industrial operators.
Traditional PLC conveyors rely on hardcoded conditional logic (e.g., IF sensor triggered THEN stop motor). AI-controlled systems integrate real-time computer vision, edge neural networks, and self-learning algorithms. They continuously adjust vector speeds, optimize item spacing, dynamically route parcel traffic during peak surges, and predict mechanical wear (such as bearing overheating or belt misalignment) before failures occur.
Yes. Our control systems support open API architectures, OPC UA, Modbus TCP/IP, and RESTful communication protocols. Our edge systems interface natively with SAP, Oracle WMS, Manhattan Associates, and custom enterprise ERPs serving facilities in Santana, ensuring instantaneous data sync for barcode tracking, item counting, and dynamic sorting.
We supply systems equipped with IP66/IP69K sealed bearing housings, self-lubricating stainless steel rollers, enclosed powder vacuum transfer pipes, and real-time vibration/thermal telemetry sensors. The AI system alerts operators in Santana of abnormal friction levels weeks prior to potential bearing seizure, allowing scheduled maintenance during non-production hours.
Most Santana logistics hubs and manufacturing facilities achieve full capital ROI within 11 to 18 months. ROI is driven by a 30–50% reduction in sorting error rates, up to 45% electricity savings through dynamic motor control, lower labor dependence during peak shifts, and the total elimination of unplanned operational downtime.
Consult directly with Hangzhou Maith Conveyor's senior automation engineering team. We offer complimentary CAD 3D layout simulation, custom AI vision integration planning, and direct factory pricing.
Send Inquiry Now Maith Conveyor