How to Improve Efficiency with China Best Conveyors? This question matters when every delayed carton creates another crowded aisle, missed dispatch, or tired worker. Conveyors can improve warehouse flow, but only when they match real operating conditions.
Joseph F. Coyle, a respected logistics scholar, described the objective clearly: “The right product, in the right quantity, at the right time, at the right place, in the right condition, at the right cost.” His principle helps explain how to improve warehouse efficiency with conveyors. A conveyor should not simply move boxes faster. It should reduce unnecessary walking, control handoffs, and support accurate order timing.
Consider a packing area where cartons arrive every 12 seconds. If the belt runs too slowly, work queues build near the scanners. If it runs too quickly, operators reach, twist, and make avoidable errors. Small details matter. Roller spacing must suit carton size. Sensors need clean lenses. Emergency stops should remain visible and accessible. These choices reflect practical engineering, not attractive catalog claims.
China-made conveyor systems can offer flexible designs and competitive production capacity. However, efficiency depends on verified load ratings, motor quality, control integration, maintenance access, and supplier support. A low purchase price may become expensive after repeated stoppages. That risk deserves attention.
There is no universal layout. Warehouse volume, SKU variety, ceiling height, labor skills, and future expansion all influence the result. This guide examines conveyor selection, layout planning, automation, safety, maintenance, and measurable performance. Some recommendations may need adjustment after testing. That is normal. Real improvement begins with honest observation.
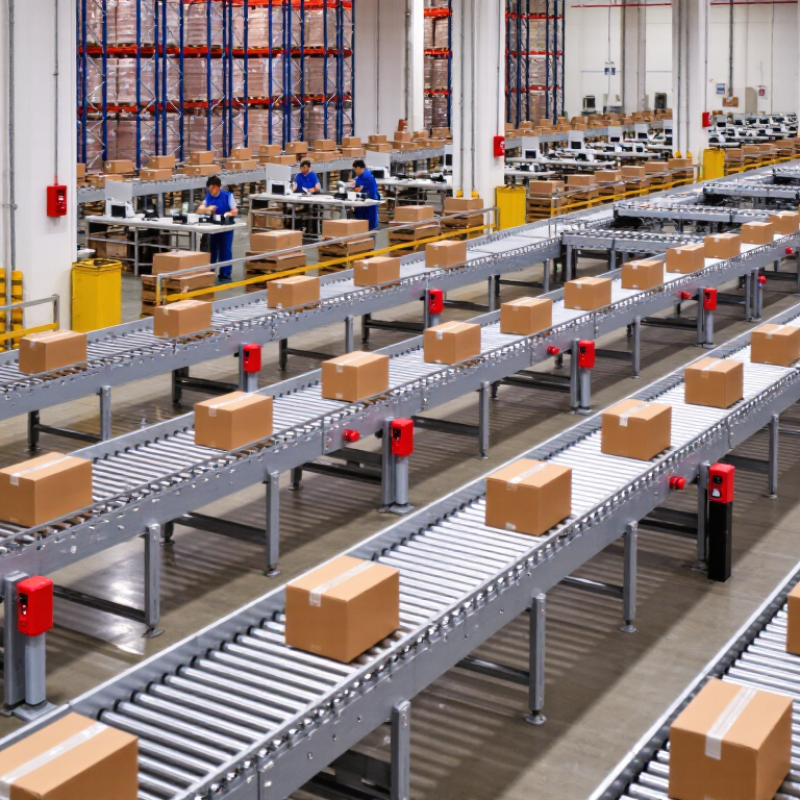
China’s best conveyors improve operational efficiency through controlled movement, not simple speed. A well-designed line keeps cartons flowing between receiving, storage, and packing areas. It reduces manual carrying, waiting time, and unnecessary forklift traffic. In my experience, the largest gains often come from layout accuracy. A fast conveyor in the wrong position creates new delays.
The International Energy Agency reports that electric motor systems consume about 50% of global electricity. Efficient conveyor motors, variable-speed drives, and automatic standby modes can therefore reduce energy waste. China’s advanced conveyor systems often combine photoelectric sensors, modular belts, and real-time monitoring. These features adjust movement when cartons accumulate. They also help maintenance teams identify abnormal noise, heat, or belt tension before failure. MHI’s 2024 Annual Industry Report indicates that 55% of supply-chain leaders planned to increase technology investment. That trend supports more connected material-handling systems.
Still, automation is not automatically efficient. Poor sensor placement can cause repeated stops. Weak operator training can reduce the value of expensive controls. A practical evaluation should measure throughput, energy use, stoppage minutes, and maintenance response time. A 10% speed increase may look impressive, but it can damage fragile goods or overload packing stations. The better approach is gradual testing, followed by adjustments based on actual shift data. Some installations need more manual observation than expected. That is a useful imperfection, not a failure.
How to Improve Efficiency with China Best Conveyors?
Identifying the right conveyor starts with the material, not the machine price. Powder, cartons, hot parts, and sharp aggregates behave differently during transport. Belt conveyors suit continuous movement and moderate loads. Roller conveyors work well for rigid boxes with flat bases. Screw conveyors can handle powders, but moisture may cause clogging. Bucket elevators help move bulk materials vertically through limited floor space.
Measure the material carefully. Record weight, size, temperature, moisture, and required speed. A conveyor carrying fragile packages needs gentle acceleration and controlled transfers. Heavy bulk material may require reinforced belts, stronger frames, and impact beds. In practical site reviews, small details often decide reliability. A narrow loading point can create spills and unnecessary cleaning. I would not select equipment from capacity figures alone.
Tips: Ask for a test using your actual material. Check belt width, motor load, emergency stops, guarding, and cleaning access. Confirm spare-part availability and maintenance instructions before purchasing. Leave room for future capacity, but avoid excessive oversizing. It increases energy use and installation costs. A useful inspection includes watching the conveyor during startup, normal loading, and shutdown. The first design may look efficient. It may still need adjustment.
Identifying the right conveyor type starts with the material, required throughput, load format, and operating environment. The chart compares representative throughput capacities for common conveyor categories used in material handling.
Belt conveyors are generally suited to continuous bulk movement and high-volume transport. Roller and chain conveyors are commonly used for cartons, pallets, and unit loads, while screw and bucket conveyors are more suitable for controlled bulk handling and vertical lifting. Actual capacity depends on material density, conveyor width, speed, incline, loading method, and safety requirements.
How to Improve Efficiency with China Best Conveyors?
Evaluating Conveyor Design, Capacity, and Energy Performance
Efficient conveyors begin with the material, not the motor. Engineers should record load weight, particle size, moisture, and transfer frequency. A belt carrying damp ore needs different pulleys than one moving sealed cartons. Small details matter.
A practical capacity review compares peak demand with rated throughput. For example, a line moving 80 tons per hour should not operate continuously at its 80-ton limit. A 15–25% reserve can reduce blockages and shorten restart delays. Belt width, incline angle, roller spacing, and loading points also affect performance. Poor alignment creates edge wear and increases maintenance visits. It happens more often than expected.
Energy performance requires measurement during real production. Check motor power, belt speed, idle running time, and starts per hour. Variable-speed drives can reduce consumption when demand changes. However, they are not a universal fix. An oversized motor may waste energy, even when the conveyor appears reliable. A simple power meter can reveal this problem within one shift.
Design reviews should include guarding, emergency stops, access platforms, and dust control. These features support safer operation and more dependable inspections. Request load tests, weld inspection records, electrical documentation, and maintenance instructions from the manufacturer. Factory acceptance testing is useful, but site conditions can expose weaknesses. Temperature, dust, and uneven foundations may change results. Engineers should compare tested performance with measured operating data after installation.
How to Improve Efficiency with China Best Conveyors?
Efficient conveyor performance begins before installation. Measure aisle widths, loading heights, walking paths, and peak carton volume on site. A five-centimeter mismatch can create repeated jams. Verify belt speed with actual products, not empty trays. Deloitte’s 2024 Smart Manufacturing and Operations Survey found that 86% of manufacturers expect smart operations to become a major competitiveness driver within five years.
Automation should solve a measured problem. Add sensors for accumulation, barcode tracking, and automatic speed adjustment where delays are visible. Connect the conveyor controller with warehouse management and production systems through clear data standards. MHI’s 2024 Annual Industry Report identifies labor availability as a continuing supply-chain challenge, making practical automation increasingly valuable. Yet full automation is not always efficient. It can increase maintenance complexity when product sizes change frequently.
Workflow integration needs disciplined testing. Run empty-load checks, then mixed-load trials during the busiest shift. Record stoppages, recovery time, energy use, and operator interventions. A useful target is reducing manual touches, not simply increasing speed. In my experience, teams often underestimate handoff points between conveyors and packing stations. That is where small delays multiply. Leave space for maintenance access, label every emergency stop, and review the layout after two weeks of real operation. The first design is rarely perfect.
How to Improve Efficiency with China Best Conveyors?
Maintaining Conveyor Systems for Long-Term Efficiency Gains
A well-built conveyor cannot stay efficient without disciplined maintenance. Daily inspections should check belt tracking, splice condition, rollers, guards, and unusual noise. Small noises matter. A loose bearing can increase friction before failure becomes visible. Operators should record these observations immediately, not rely on memory.
Weekly maintenance can include cleaning material buildup around pulleys and removing dust from sensors. Technicians should measure belt tension with suitable tools, rather than tightening it by feel. Excessive tension may damage bearings and increase energy use. Correct alignment also protects the belt edges from premature wear. Follow the conveyor supplier’s manual and site safety procedures during every adjustment.
Maintenance records should show inspection dates, detected faults, replaced parts, and operating conditions. This history helps teams identify repeated problems, such as loading imbalance or moisture-related slippage. Do not guess. Compare vibration, temperature, and motor current with earlier readings. A practical weakness is often overlooked: teams may inspect visible components but ignore transfer points beneath the frame. Reviewing this blind area can reveal hardened material, hidden corrosion, or a roller that turns unevenly. Regular training keeps these checks consistent, especially when different operators share the same system.
| Maintenance Area | Recommended Frequency | What to Check | Practical Performance Target | Efficiency Benefit | Early Warning Signs |
|---|---|---|---|---|---|
| Visual inspection | Before each operating shift | Inspect belts, rollers, guards, fasteners, transfer points, and material buildup. | No visible damage, loose components, or blocked transfer points | Identifies small defects before they develop into unplanned stoppages. | Frayed belt edges, unusual noise, loose guards, spilled material, or tracking drift |
| Belt alignment and tracking | Weekly and after belt or roller replacement | Check idlers, pulleys, loading alignment, belt tension, and side-to-side belt movement. | Belt remains centered under normal load | Reduces edge damage, product spillage, and belt wear. | Repeated contact with the structure, uneven belt wear, or material falling from one side |
| Roller and idler condition | Weekly; inspect more often in dusty or abrasive environments | Check for seized bearings, excessive vibration, damaged shells, and free rotation. | All rollers rotate smoothly without abnormal noise or heat | Reduces rolling resistance and protects the belt from localized wear. | Grinding sounds, hot bearing housings, visible wobble, or a roller that does not rotate |
| Lubrication | According to the component manufacturer's schedule | Lubricate approved bearings, drive components, and tensioning mechanisms using the specified lubricant. | Correct lubricant, quantity, and interval recorded in the maintenance log | Helps control friction, heat generation, and premature bearing failure. | Dry fittings, grease leakage, rising bearing temperature, or lubricant contamination |
| Drive motor and gearbox | Monthly | Inspect mounting bolts, couplings, oil level, ventilation openings, vibration, and operating temperature. | No abnormal vibration, overheating, leakage, or mounting movement | Maintains stable conveying speed and reduces drive-related downtime. | Oil leaks, burnt odor, high noise, repeated overload trips, or speed fluctuations |
| Belt tension | Monthly and after initial belt installation | Verify tension against the conveyor design requirements and inspect take-up travel. | Enough tension for traction without excessive belt stress | Limits slipping, power waste, belt stretching, and pulley wear. | Belt slip during startup, excessive sag, frequent retensioning, or high motor current |
| Electrical and safety devices | Monthly; test emergency devices according to site procedures | Test emergency stops, pull-cord switches, guards, interlocks, sensors, and cable condition. | All protective devices respond correctly during every documented test | Supports safe operation and prevents extended outages caused by unnoticed control faults. | Intermittent sensor signals, damaged cables, failed indicator lights, or delayed emergency-stop response |
| Spillage and carryback control | Daily cleaning; detailed review weekly | Inspect skirt seals, belt cleaners, chutes, scrapers, and transfer-point containment. | No recurring buildup that interferes with rollers, walkways, or sensors | Improves housekeeping, reduces cleanup labor, and protects moving components. | Material accumulation under the conveyor, blocked chutes, dust clouds, or frequent manual cleanup |
| Belt splice and fasteners | Monthly and after any abnormal overload | Examine splice edges, fasteners, bonding, cover separation, and local deformation. | Splice remains flat, secure, and free from separation or exposed damage | Prevents sudden belt failure and reduces the risk of extended replacement downtime. | Raised splice sections, cracking, exposed fasteners, or repeated impact damage |
| Energy and operating data | Review weekly; compare monthly trends | Record motor current, operating hours, throughput, stops, alarms, and maintenance work orders. | Stable energy use and a declining trend in repeat faults | Reveals overload, friction, underutilization, and recurring maintenance problems. | Increasing current at the same load, longer start-up time, or repeated short stoppages |
| Planned component replacement | Based on inspection results and condition data | Replace worn rollers, cleaners, bearings, seals, and belts before failure limits are reached. | Critical spares available and replacement work completed during planned downtime | Converts emergency repairs into predictable maintenance activities. | Repeated temporary repairs, reduced component life, or unavailable critical spare parts |
| Maintenance documentation | Update after every inspection or repair | Record findings, measurements, parts used, downtime, root causes, and corrective actions. | Complete, dated records for all critical conveyor assets | Improves trend analysis, spare-parts planning, and maintenance accountability. | Missing inspection records, repeated unresolved faults, or inconsistent maintenance intervals |
| Maintenance intervals should be adjusted for conveyor length, load, speed, operating hours, material abrasiveness, dust, moisture, temperature, and the equipment manufacturer's instructions. | |||||
Record load weight, particle size, moisture, and transfer frequency. A damp ore load needs different pulleys than sealed cartons. Small details matter.
Compare peak demand with rated throughput. A 15–25% reserve can reduce blockages and restart delays. Running at the limit is risky.
Belt width, incline angle, roller spacing, and loading points affect capacity. Poor alignment may cause edge wear and repeated maintenance visits.
Check motor power, belt speed, idle time, and starts per hour during production. A basic power meter may reveal waste within one shift.
No. They help when demand changes, but they are not a universal fix. An oversized motor can waste energy while appearing reliable.
Inspect guarding, emergency stops, access platforms, and dust-control measures. These features support safer inspections and steadier operation.
Inspect belt tracking, splices, rollers, guards, and unusual noise. Small noises matter. A loose bearing may increase friction before failure appears.
Record inspection dates, faults, replaced parts, and operating conditions. Compare vibration, temperature, and motor current with earlier readings. Do not guess.
Inspect transfer points beneath the frame, not only visible components. Hidden buildup, corrosion, or uneven rollers may remain there. This weakness is easy to miss.
No. Site temperature, dust, and uneven foundations may change results. Compare factory results with measured operating data after installation. The review may still miss something.
Improving efficiency with China’s best conveyors starts with understanding how the right system can streamline material movement, reduce manual handling, and support consistent throughput. Businesses should select conveyor types based on material size, weight, shape, and movement requirements. They should also evaluate design features such as capacity, layout flexibility, durability, and energy performance to ensure the equipment matches current operations while allowing room for future growth. These factors are essential when considering how to improve warehouse efficiency with conveyors.
Effective results also depend on professional installation, suitable automation, and smooth integration with storage, picking, packing, and dispatch workflows. Sensors, controls, and data monitoring can help reduce delays and improve process visibility. Regular inspections, cleaning, lubrication, belt or roller adjustments, and timely replacement of worn components are equally important. With thoughtful planning and preventive maintenance, conveyor systems can deliver safer operations, lower operating costs, and long-term efficiency improvements.
Maith Conveyor